About Industrial Methylbenzene
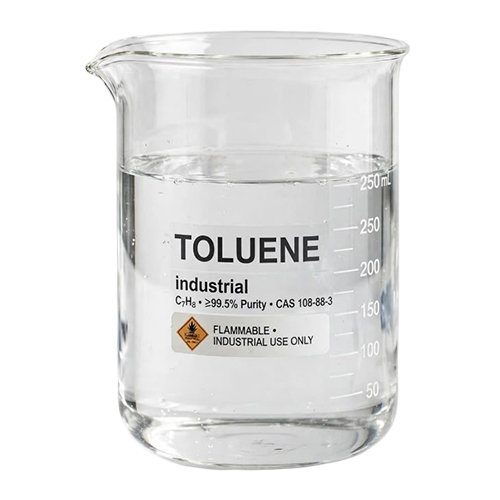
Seize this Promotion and Pick Yours today-Industrial Methylbenzene (Toluene) at an Unbeatable Price! Experience the Terrific quality and Glorious purity (99.9%) of this distinguished aromatic hydrocarbon. Boasting technical parameters like a 110.6C boiling point, 6C flash point, and 28.4 mmHg vapor pressure at 25C, it is perfect for use as a solvent, paint thinner, or in chemical synthesis. Presented as a clear, colorless liquid, packaged in drums, cans, or bulk, this industrial-grade toluene delivers exceptional strength. Safety first-handle with care and adhere to hazardous material guidelines.
Features & Application Areas of Industrial Methylbenzene
Industrial Methylbenzene, also known as Toluene, is revered for its distinguished performance as a solvent in paints, adhesives, and chemical synthesis. This product stands out with a glorious purity of 99.9% and rapid evaporation. Its versatility makes it ideal for manufacturers, suppliers, and traders who require industrial-grade strength. Being volatile and flammable, it is expertly suited for sectors demanding fast-drying and high-quality solvent solutions. Always apply as directed in well-ventilated processing areas.
FOB Port, Export Markets & Domestic Reach for Methylbenzene
Our Industrial Methylbenzene is available for Drop-off at multiple Indian FOB ports, ensuring convenient logistics. The list price is competitive, reflecting the product's unmatched quality for bulk buyers. India is our principal domestic market, with significant export markets in Asia, the Middle East, and Africa. Whether for manufacturers or traders, we guarantee smooth delivery and prompt handling, making us a trusted supplier both locally and in the global export market.
FAQ's of Industrial Methylbenzene:
Q: How should Industrial Methylbenzene be safely handled and stored?
A: Industrial Methylbenzene must be handled with protective gear, such as gloves and goggles, in a well-ventilated area. Store it in tightly sealed containers in a cool, dry, ventilated space to minimize vapor accumulation and the risk of fire.
Q: What are the primary industrial applications of Methylbenzene?
A: Methylbenzene is widely used as a solvent in paints, adhesives, and chemical manufacturing, owing to its fast evaporation and impressive solvency power. It is also utilized in the synthesis of other chemicals in industrial settings.
Q: Where is your main export market for Industrial Methylbenzene?
A: Our main export markets include countries in Asia, the Middle East, and Africa, with India being the principal domestic market.
Q: What are the benefits of using Industrial Methylbenzene in manufacturing?
A: Industrial Methylbenzene provides excellent solubility for a wide range of substances, enhances drying times due to its volatility, and ensures high purity, making it a preferred choice for quality-sensitive industries.
Q: When does Industrial Methylbenzene reach its expiry or require replacement?
A: This product has a shelf life of one year from the date of manufacture, after which quality may decline and replacement is recommended for optimal results.
Q: How is Methylbenzene transported and what are the packing options?
A: It is classified as a hazardous material under UN 1294 and is packed in secure drums, cans, or bulk containers for both domestic and international transport, complying with safety regulations.



 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
